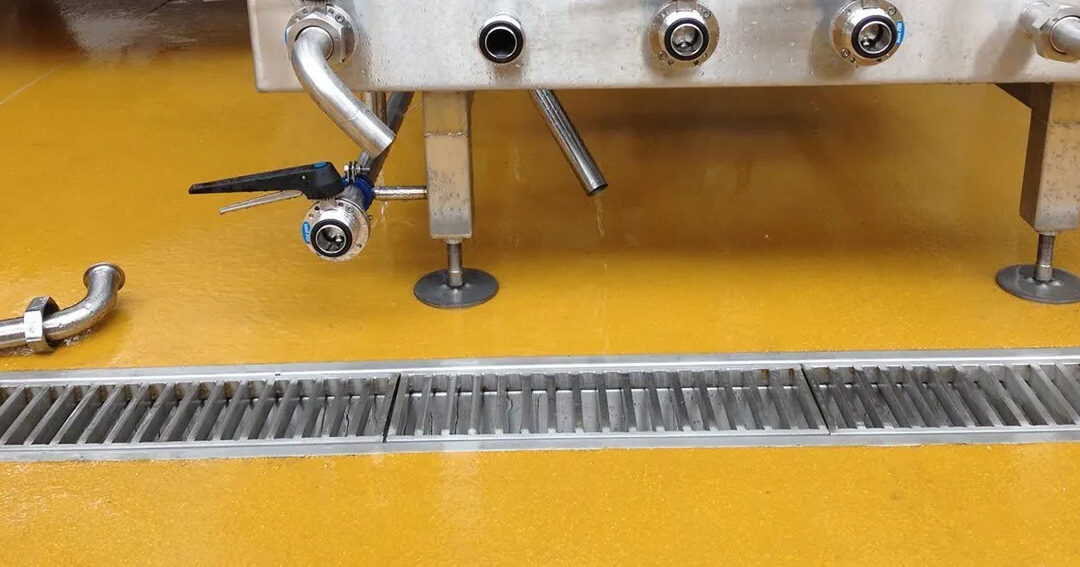
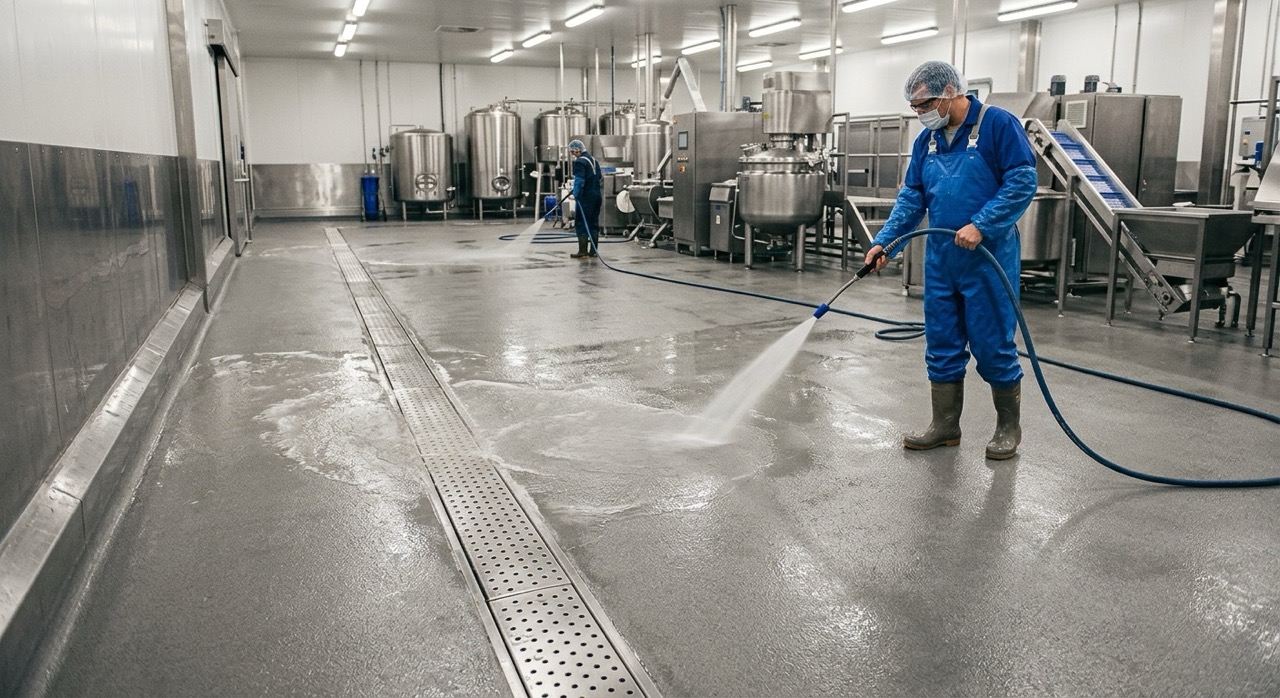
Selecting the right food grade flooring is one of the most critical decisions for any commercial kitchen, processing plant, or beverage facility across Australia. Flooring in food production zones must endure extreme thermal shock, frequent hot water washdowns, aggressive organic acids, and heavy wheeled traffic—all while maintaining strict health and safety compliance.
At Diamond Grind, we consistently specify polyurethane cement screeds for facilities that cannot afford floor failures. While traditional concrete sealers and standard coatings break down under harsh operational demands, high-performance polyurethane cement creates a dense, non-porous, hygienic barrier built for long service life. Here is why polyurethane cement is the gold standard for heavy-duty commercial food environments.
What Is Polyurethane Cement Screed?
Polyurethane cement (often referred to as PU cement or polyurethane mortared screed) is a specialized 4-part resin system composed of polyurethane resin, reactive hardeners, aggregate fillers, and cementitious binders. Unlike thin-film paint coatings, polyurethane cement is applied at heavy-duty thicknesses ranging from 3mm to 9mm.
When applied over mechanically prepared concrete, the polymer matrix bonds deeply into the open pores of the slab. This chemical and mechanical bond creates a seamless, non-porous floor system engineered specifically to withstand heavy impact, continuous moisture, and harsh industrial sanitizers.
Key Advantages of Polyurethane Cement Food Grade Flooring
For facility managers and business owners evaluating long-term surface protection, polyurethane cement delivers distinct physical and operational benefits over alternative materials.
1. Exceptional Thermal Shock Immunity
In food grade flooring facilities with steam cleaning lines, industrial ovens, or walk-in freezers, rapid temperature fluctuations cause standard floors to expand and contract at a different rate than the underlying concrete slab, leading to delamination. Polyurethane cement expands and contracts at a thermal rate similar to concrete, enduring direct steam washdowns and boiling liquids up to 120°C without cracking, blistering, or peeling.
2. Hygiene Built for HACCP Programs
Contamination control is essential in food production. Polyurethane cement forms a seamless, non-porous surface with zero grout lines or seams where bacteria, mould, and fungi can colonize. These systems comply fully with Australian Food Safety Standards and HACCP compliance requirements, ensuring your facility passes council health inspections effortlessly.
3. Resistance to Organic Acids, Fats, and Cleaners
Food processing generates destructive byproducts—including lactic acids in dairy production, animal fats in meat processing, and citric acids in beverage plants—that rapidly erode standard concrete. Polyurethane cement offers exceptional chemical resistance against harsh acids, alkalis, fats, and industrial cleaning detergents.
4. Anti-Slip Safety in Wet Zones
Slips and falls are among the highest workplace risks in commercial kitchens and processing washdown areas. Polyurethane cement can be customized with textured aggregate profiles designed to achieve anti-slip ratings up to P5 under Australian Standards, maintaining foot traction even when covered in water, oils, or food waste.
5. Superior Mechanical Bond and Moisture Tolerance
Unlike epoxy coatings that require completely dry concrete to cure, high-grade polyurethane cement exhibits excellent tolerance to moisture vapor within the slab. This makes it an ideal option for fast-turnaround refurbishment projects where damp concrete or tight operational schedules prevent lengthy drying times.
Where Is Polyurethane Cement Installed as Food Grade Flooring?
Because of its resilience and hygienic properties, this system is widely installed across high-traffic, compliance-heavy commercial environments:
- Commercial Kitchens & Restaurants: Under heavy cooking lines, deep fryers, dishwashing pits, and prep stations.
- Food Processing & Manufacturing: Meat abattoirs, seafood handling rooms, bakeries, and dairy facilities.
- Beverage Production: Craft breweries, wineries, bottling plants, and soft drink manufacturing hubs.
- Cold Storage & Distribution: Blast freezers, cold rooms, and climate-controlled warehouse facilities.
Epoxy vs. Polyurethane Cement: Which System Wins?
While both systems belong to the resin family, their performance in active food environments differs significantly:
- Standard Epoxy Coatings: Excellent for dry industrial zones, automotive workshops, and showrooms. However, epoxy can soften when exposed to temperatures exceeding 60°C and is vulnerable to cracking under thermal shock or heavy impact.
- Polyurethane Cement Screeds: Purpose-built for wet, hot, and aggressively cleaned zones. It handles extreme heat, heavy impact from dropped equipment, and harsh organic chemical exposure that would otherwise destroy standard epoxy. Learn more about selecting the right specification in our full polyurethane cement flooring guide.
Professional Preparation and Technical Installation
A high-performance floor system is only as reliable as the mechanical floor preparation behind it. At Diamond Grind, we prepare concrete substrates using dust-free diamond grinding and shot-blasting to open the concrete surface profile, establishing an unbreakable bond before trowelling the polyurethane matrix.
Investing in experienced trade specialists ensures correct slope-to-drain alignment, proper termination coving along walls, and seamless integration around stainless steel drainage channels.
Food Grade Flooring FAQs
What makes polyurethane cement the best food grade flooring for commercial kitchens?
Polyurethane cement is widely considered the ultimate food grade flooring because it is completely seamless, resistant to thermal shock up to 120°C, highly slip-resistant, and immune to organic acids, oils, and fats. Its non-porous structure leaves bacteria nowhere to hide, which supports HACCP food safety programs.
How thick is food grade polyurethane cement installed?
Polyurethane cement food grade flooring is typically installed at a heavy-duty thickness between 3mm and 9mm. The required thickness depends on operational exposure; 3mm to 4mm is ideal for general wet processing, while 6mm to 9mm is required for areas subjected to extreme thermal shock, steam cleaning, and heavy machinery traffic.
Can polyurethane cement be applied over damp or old concrete?
Yes. Unlike traditional epoxy coatings that require completely dry concrete, polyurethane cement screeds exhibit high tolerance to substrate moisture and adhere exceptionally well to damp concrete slabs. This makes it ideal for fast-turnaround refurbishments in existing food processing plants.
How long does a polyurethane cement floor last in a food facility?
When professionally prepared and installed by experienced contractors, a polyurethane cement floor can last up to 15 to 20 years or more, even under continuous heavy impact, boiling water washdowns, and harsh chemical cleaning routines.
✅ Let's Talk — DiamondGrind
100% free consultation — no commitment required.